Task:End machining of pipes up to 14 m long |
Workpieces:Pipes for the oil and gas industry |
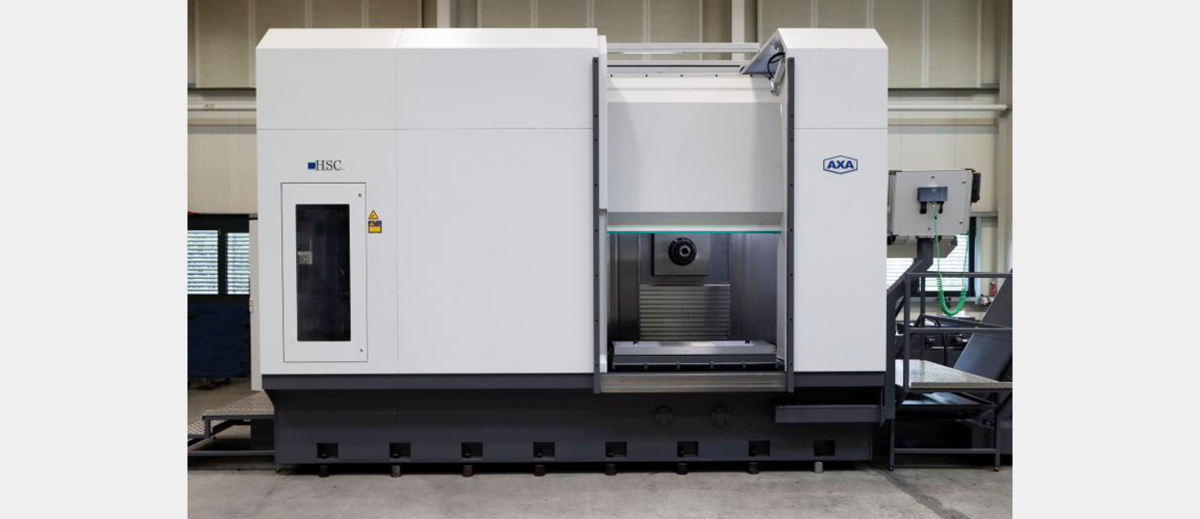
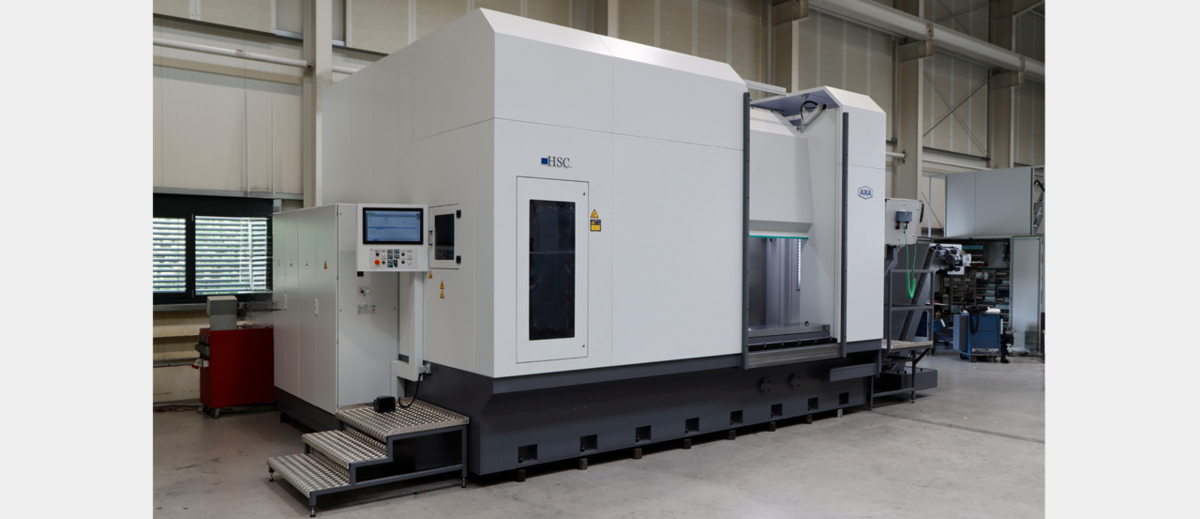
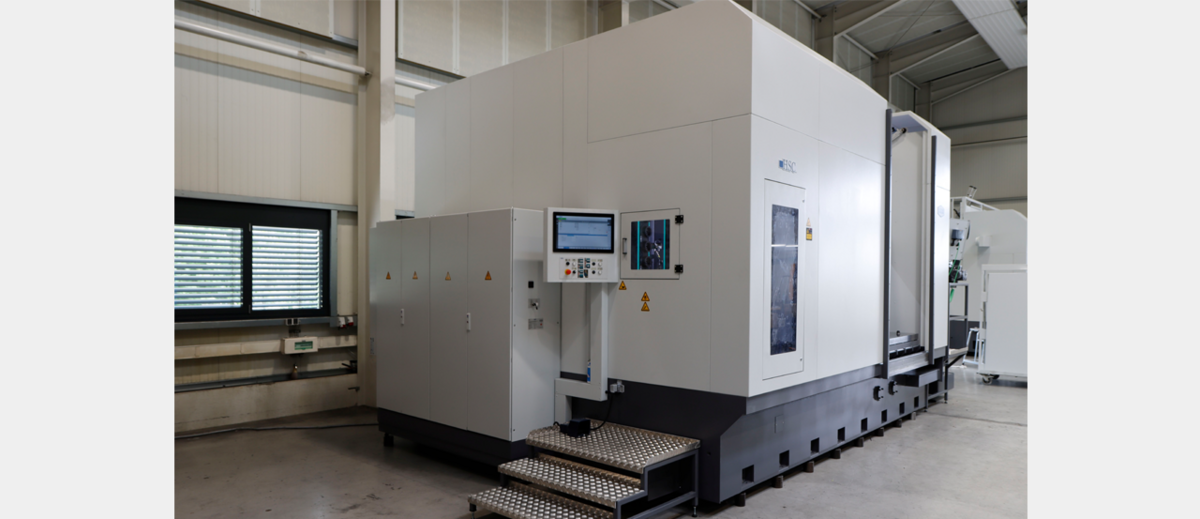
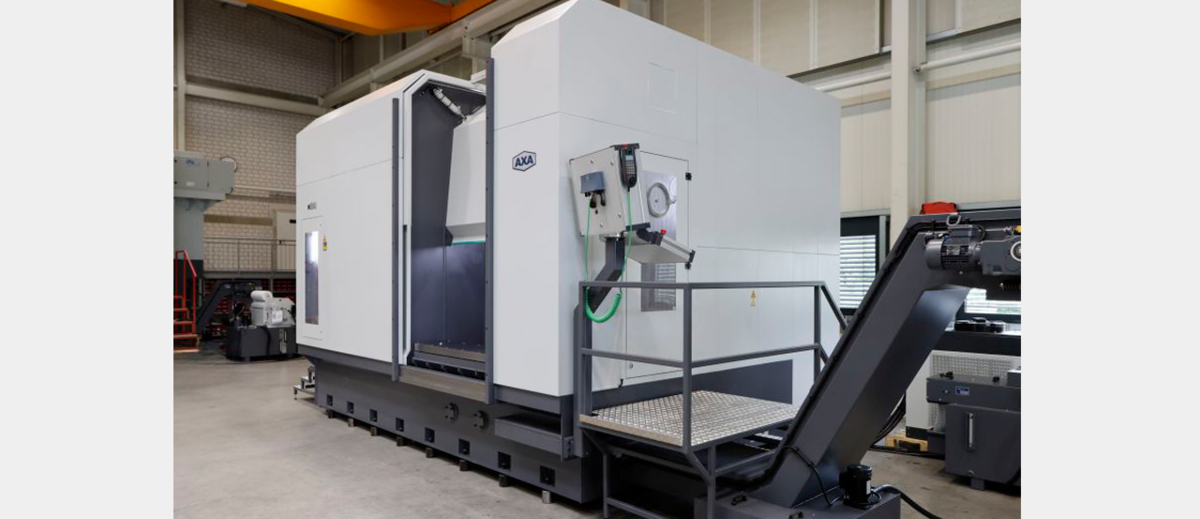
Solution:- Use of the HSC model with a horizontal spindle.
- A base plate is integrated into the machine column to support the workpieces. The pipe is clamped using a customer-supplied clamping fixture.
- A swivelling panel closes flush with the clamping fixture, so that only the end of the pipe protrudes into the working area during machining.
|
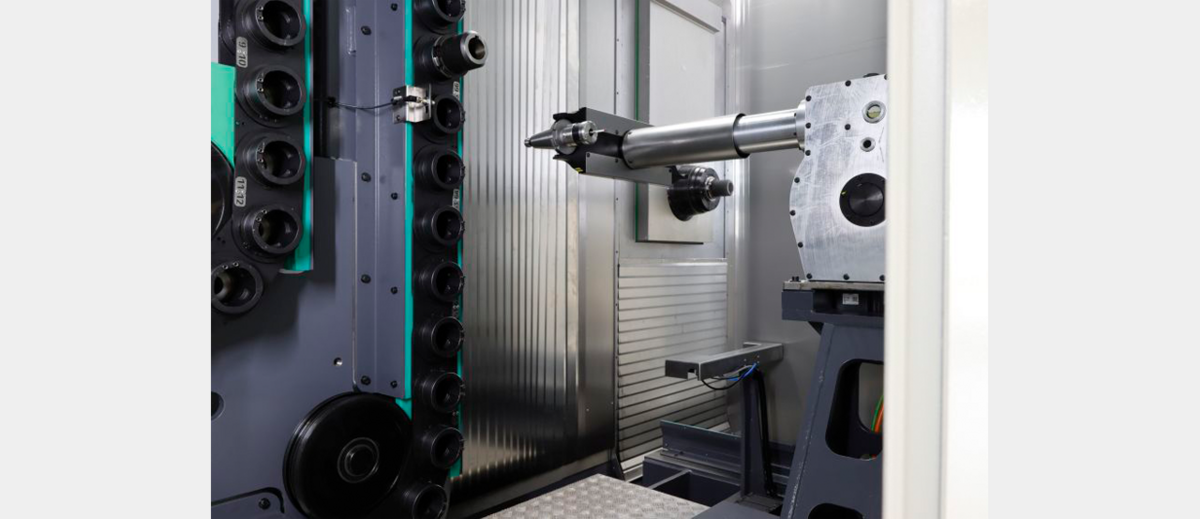
Special features:- Vertically mounted chain magazine with 80 tool pockets
- Tool change via an intermediate double gripper
- An additional swivelling partition is fitted in the working area to keep chips and coolant inside the machine.
|
Working area:X-traverse range: 1000 mm
Y-traverse range: 1000 mm
Z-traverse range: 900 mm |
Clamping surface:Base plate measuring 1400 × 400 mm |
Spindle:Power (with 100% DC): max. 81 kW
Torque (with 100% DC): max. 820 Nm
Speed range: 4000 rpm |
Tool changing system:Vertical chain magazine with 80 tool pockets, SK50
with double gripper |
CNC-system:Siemens Sinumerik ONE |
Additional equipment:- Recooling unit
- Fully enclosed working area
- Side access door
- Rotating viewing window
- Renishaw RMP60 touch probe
- BLUM Micro Compact NT laser tool measurement system
- Tool monitoring by means of active power measurement / limitation
- Balluff tool identification system with read/write station
- OPC UA software interface
- Robot interface
- Operating mode 3 without an enabling switch
- belt filter system with 800 l tank
|